Equipment scope · viewed through daily factory operation
Water Bottling Factory Equipment: Complete Line and Supplier Checklist
Select water bottling factory equipment as one connected system, then qualify the supplier through itemized scope, interface data, documented tests, acceptance rules, installation responsibilities and lifecycle-support evidence.
Catalog evidence · reference, not final specification
Equipment references within the factory operating system
The following values come from the 2026 Allot Tech beverage bottling catalog and require project-specific reconfirmation.
PET water rinsing-filling-capping
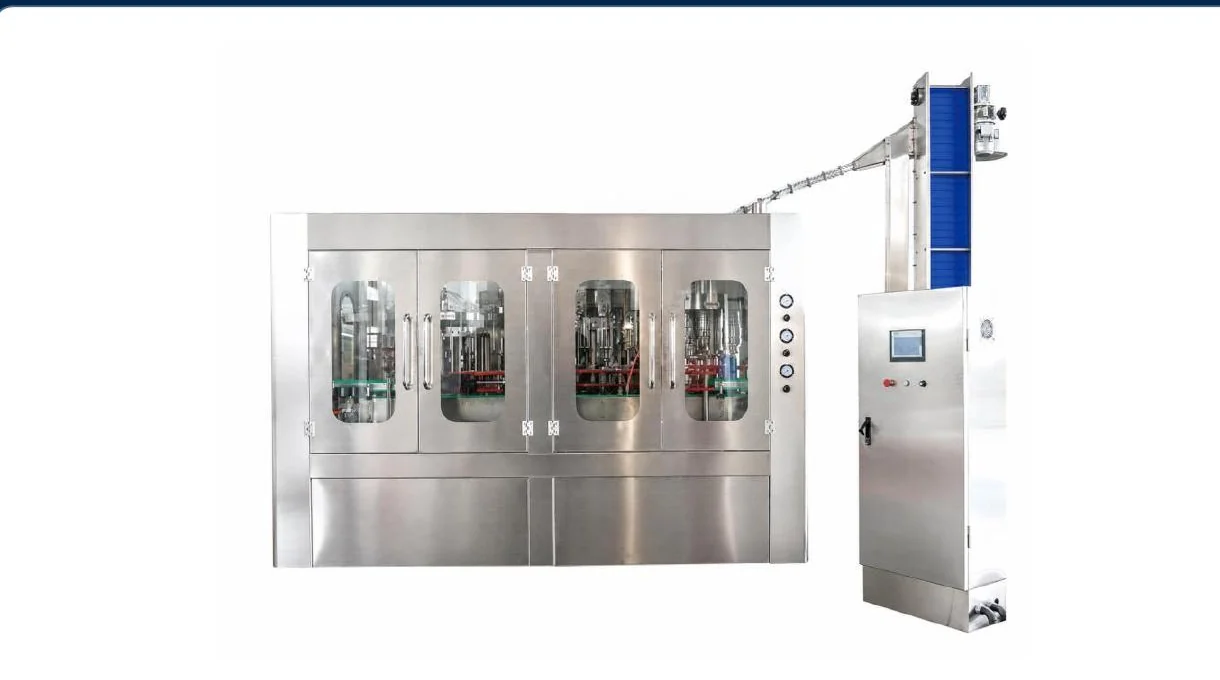
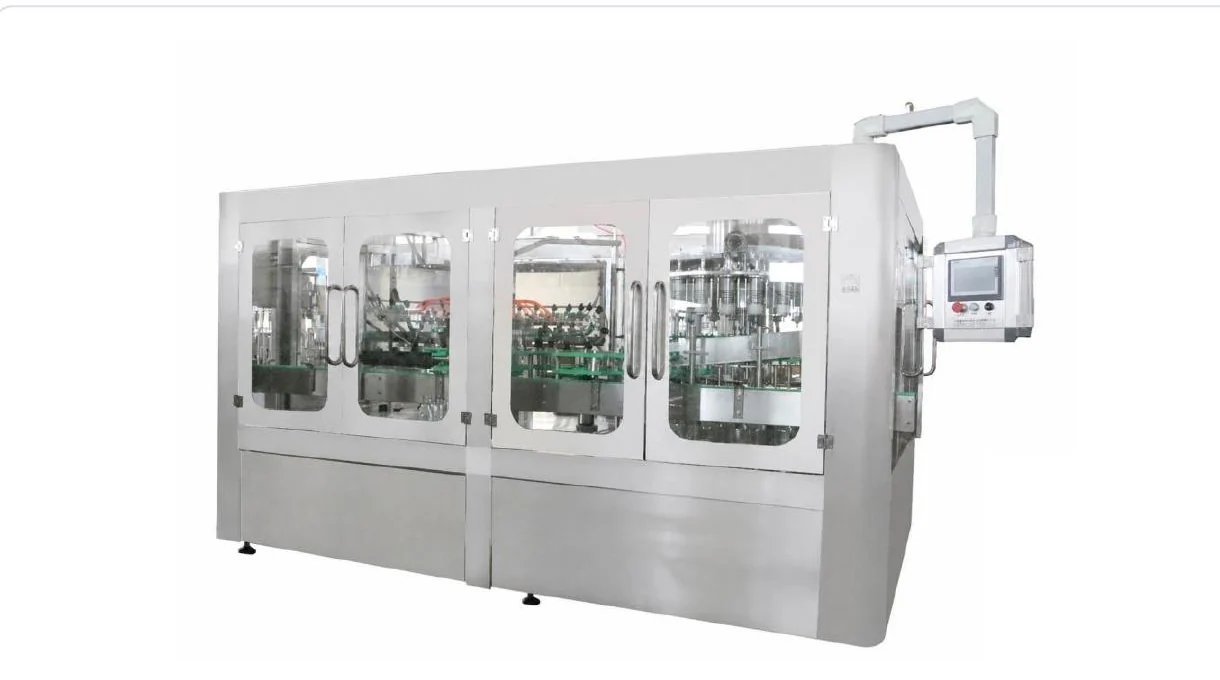
The 2026 Allot Tech catalog shows XGF three-in-one water filling references across 6,000–42,000 BPH on catalog pages 9–10. Final performance depends on the confirmed project basis.
REFERENCE · REQUIRES CONFIRMATIONLarger PET formats
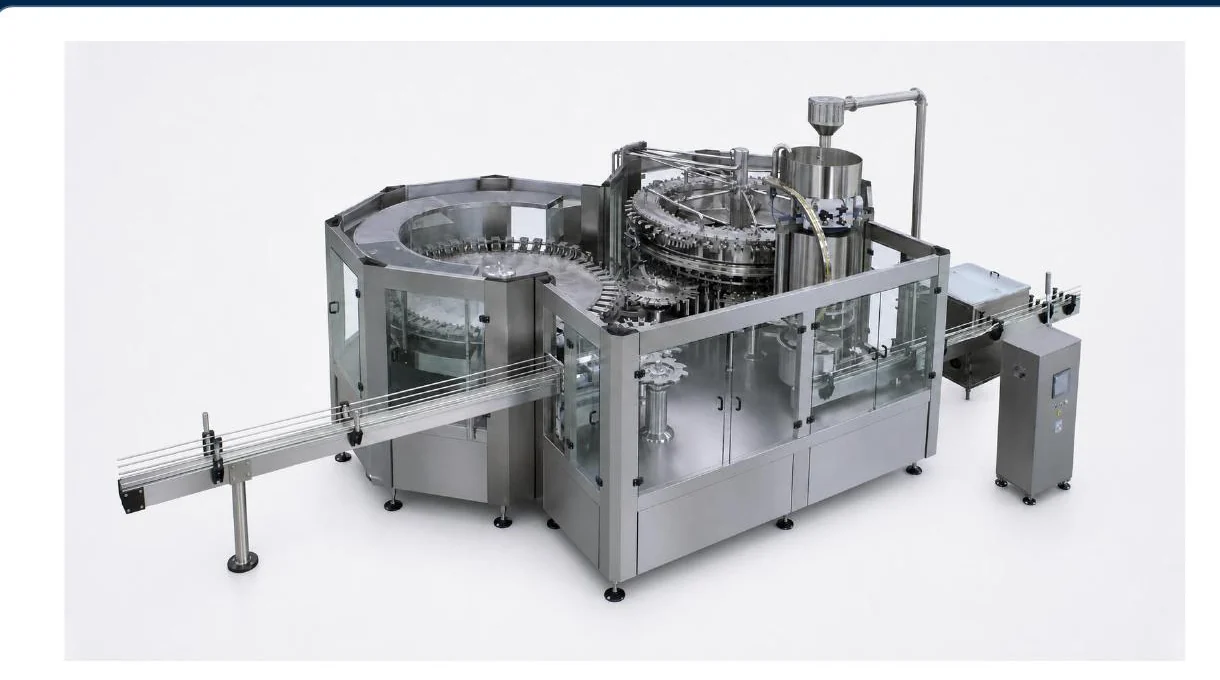
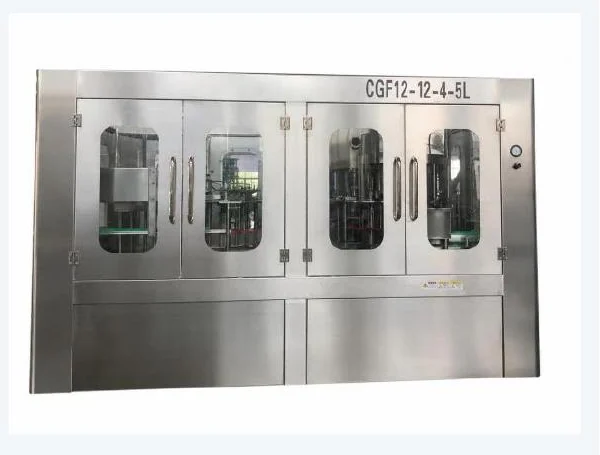
Catalog page 20 presents 3–15 L rotary and 3–10 L linear/piston filling references. Bottle, closure, output and exact configuration require confirmation.
REFERENCE · REQUIRES CONFIRMATIONReturnable 5-gallon route
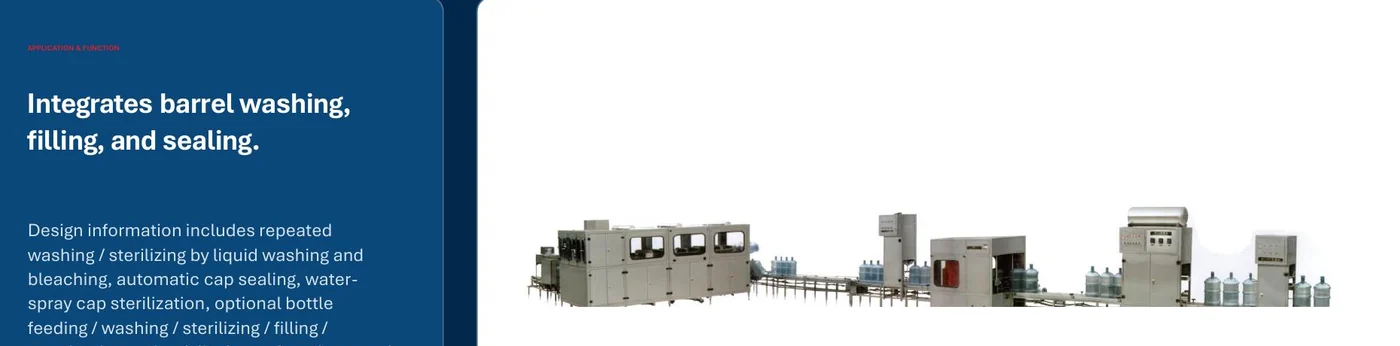
Catalog pages 21–22 present QGF 18.9 L / 5-gallon references from 60–800 bottles per hour. Several model rows require supplier reconfirmation before quotation use.
REFERENCE · REQUIRES CONFIRMATIONWater preparation and line support
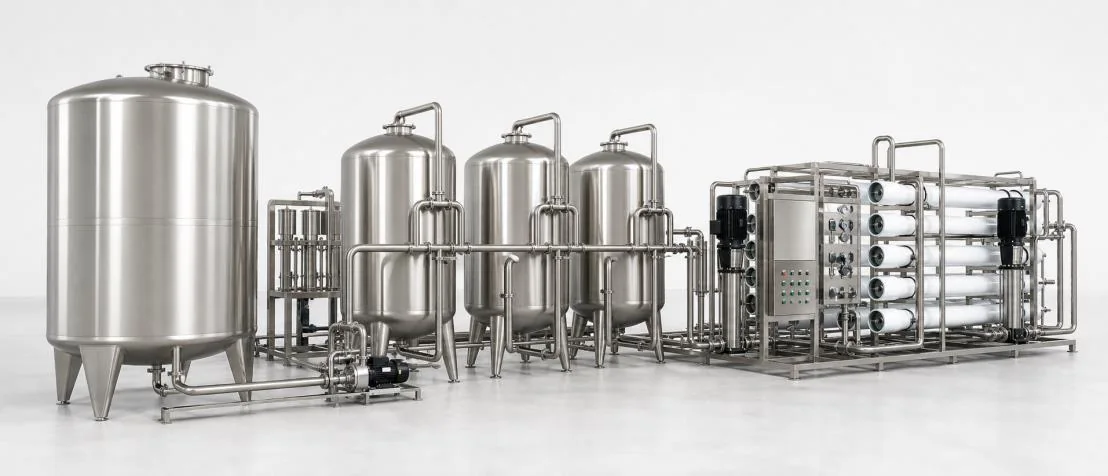
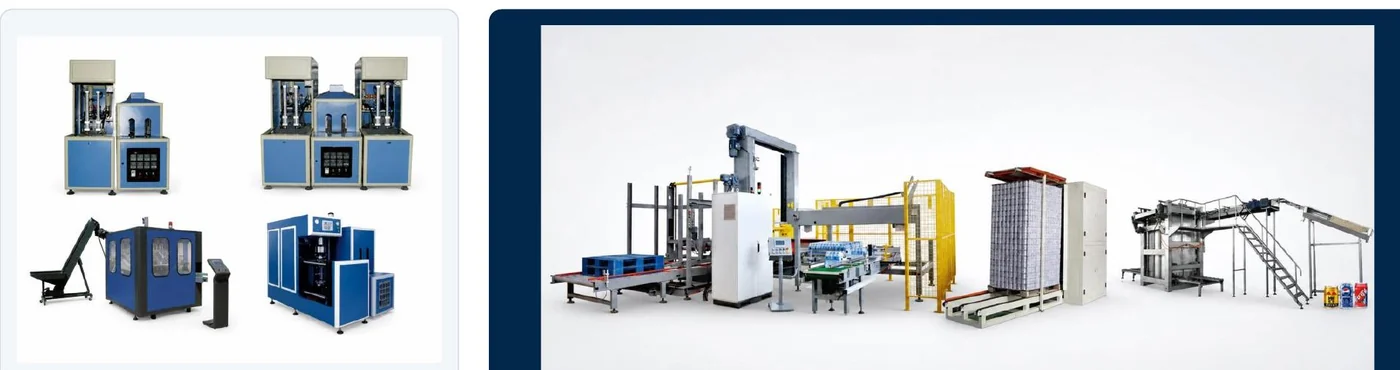
Catalog pages 28–29 and 36–37 illustrate water-treatment, RO/ultrafiltration, bottle drying and complete purified/mineral-water process references.
REFERENCE · REQUIRES CONFIRMATION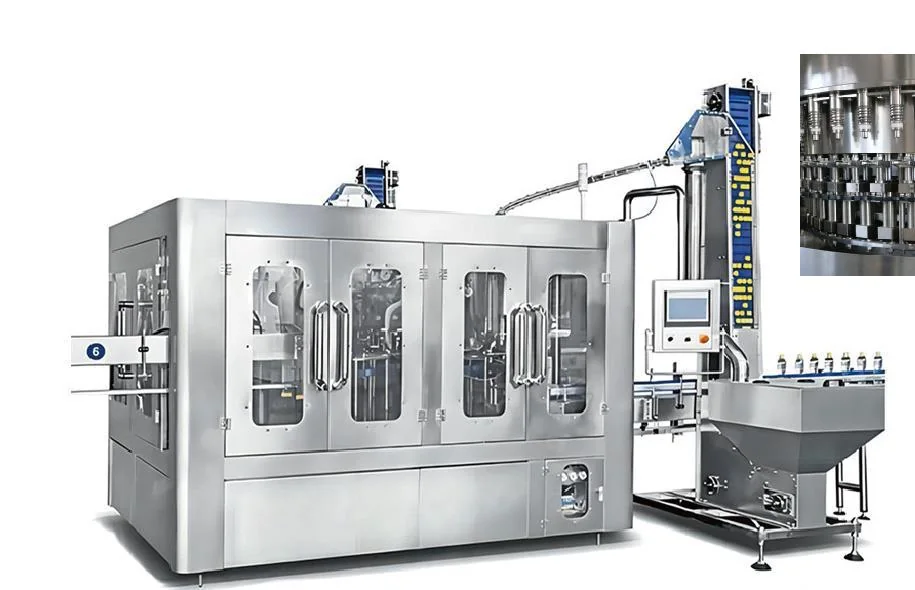





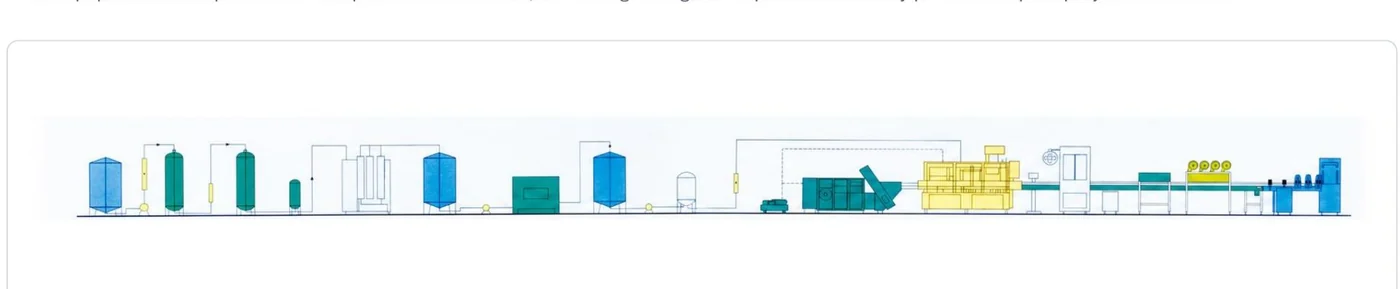
Complete factory boundary · function by function
Water Bottling Factory Equipment List and Selection Inputs
The correct equipment list follows the product and package route. The rows below define the functional chain and the data needed to select it without treating one catalog model as a universal answer.
| Factory function | Typical equipment scope | Selection inputs to confirm | Critical interface |
|---|---|---|---|
| Water preparation | Raw-water storage, pumps, pretreatment, membrane or selected treatment, disinfection and product-water storage | Water analysis, intended product, recovery basis, peak demand and sanitation method | Treatment flow and storage must support filler demand and cleaning |
| Bottle supply | Preform handling and blow molding, bottle unscrambler, or controlled empty-bottle feed | Bottle route, resin, preform, neck, volume range and damage limits | Stable bottle supply and accumulation at the filler infeed |
| Rinse, fill and cap | Monoblock or separate rinsing, filling and closing functions | Product, bottle, cap, fill basis, hygiene level and output by format | Product-water, bottles, caps, controls and discharge stability |
| Surface preparation and decoration | Bottle dryer, labeler, coder and relevant inspection | Bottle surface, label type, code content/location and reject logic | Dry and stable bottles at the confirmed line speed |
| Conveying and accumulation | Air conveyor, bottle conveyor, buffer table, pack conveyor and controls | Layout, elevations, transfer points, stop logic and recovery behavior | Line balance between modules with different stop/start patterns |
| Secondary packaging | Shrink film, tray, carton, handle or case-packing route | Pack pattern, materials, presentation, output and changeover range | Saleable filler output must pass through the packer without hidden loss |
| Pallet and warehouse handling | Palletizer, stretch wrapper, conveyors or manual handling aids | Pallet pattern, warehouse flow, load stability and dispatch method | Finished packs need controlled identification, hold and release space |
| Utilities and support | Compressors, dryers, chillers, electrical distribution, CIP, laboratory and critical spares | Measured qualities, simultaneous loads, ambient conditions and support capability | Utilities must be verified at operating load, not only by installed rating |
Supplier comparison · normalize the boundary
How to Compare Two Complete-Line Quotations
A lower total can reflect missing scope rather than lower cost. Rebuild each offer into the same comparison columns before deciding.
| Comparison test | Evidence to request | Red flag |
|---|---|---|
| Same production basis | Bottle sizes, output by format, product conditions and operating schedule | One quote uses maximum catalog speed and the other uses an accepted-line basis |
| Same equipment boundary | Itemized modules, quantities, interfaces and explicit exclusions | Conveyors, coding, inspection, dryers, compressors or packing disappear from the total |
| Same utility boundary | Consumption basis, quality, pressure, temperature and terminal points | Only installed motor power is shown without simultaneous operating demand |
| Same service boundary | Installation, commissioning, training, travel, tools and local labor split | Startup support is described generally but not priced or assigned |
| Same acceptance basis | Test product, formats, duration, measurements, output and quality disposition | A speed statement has no stated conditions or verification method |
| Same lifecycle support | Manuals, drawings, change parts, recommended and critical spares, response route | Spare and documentation scope is postponed until after the order |
Supplier qualification · evidence before commitment
How to Choose a Water Bottling Factory Equipment Supplier
A supplier should be evaluated on its ability to control the complete project boundary and prove the promised result under stated conditions. Treat sales claims as inputs to verify, not as acceptance evidence.
| Capability to qualify | Evidence to request before order | Question for the supplier | Risk if left vague |
|---|---|---|---|
| Requirement control | Dated requirement list, drawing register, open-item log and revision method | How will a bottle, cap, label, product or output change be assessed and approved? | Different teams build to different assumptions |
| Complete-line engineering | Itemized process flow, equipment list, layout, interface matrix and exclusions | Who owns the connection between treatment, blowing, filling, packing and utilities? | Individual machines arrive without a working system boundary |
| Relevant project evidence | References with comparable product, package, automation and service scope that the buyer may verify | Which parts of those references are genuinely comparable to this project? | Unrelated installations are presented as proof of project fit |
| Manufacturing and quality control | Inspection plan, material records, key assembly checks, software backup method and nonconformance route | Which build records will be supplied with the equipment? | Defects or configuration changes cannot be traced |
| Testing and acceptance | Draft FAT/SAT protocol with formats, conditions, duration, measurements, deviations and retest rules | What exactly proves completion, and what remains to be proven at site? | A short demonstration is treated as accepted production performance |
| Installation and startup support | Responsibility matrix for travel, labor, tools, lifting, utilities, materials, training and daily records | Which prerequisites stop the service clock or require extra cost? | Schedule and cost disputes appear during startup |
| Lifecycle support | Manual index, drawings, backups, change-parts list, critical spares, response channel and escalation path | What can the site team solve locally, and what requires supplier authorization? | The factory depends on undocumented knowledge after handover |
FAT to stable production · protect the handover
Define FAT, Delivery, Installation and After-Sales Before the Purchase Order
The commercial offer should connect every project stage to named inputs, records, responsibilities and completion evidence. Exact criteria remain project-specific and belong in the signed agreement.
| Project stage | Minimum written boundary | Evidence at completion | Buyer-side preparation |
|---|---|---|---|
| Design freeze | Approved product, formats, line scope, layout, utilities, interfaces, standards basis and open items | Signed revisions and a closed or owned open-item register | Provide reliable samples, drawings, site data and decision owners |
| Factory acceptance test (FAT) | Test media, formats, duration, speed basis, functional and safety checks, measurements, deviations and retest route | Signed protocol, raw observations, issue list, configuration backup and disposition | Attend with authorized technical and commercial decision-makers |
| Packing and delivery | Packing protection, marks, shipping documents, Incoterm, insurance boundary, quantities and arrival inspection route | Packing list, shipment records and receipt-condition evidence | Confirm import, unloading, storage, access and lifting responsibilities locally |
| Installation | Foundation, positioning, mechanical, electrical, utility, control and safety completion boundaries | Installation checklist, red-line drawings, connection records and open-item list | Make the building, drainage, utilities, materials, tools and safe work areas ready |
| Commissioning and SAT | Prerequisites, product and materials, formats, test sequence, quality disposition, output basis, training and acceptance decision | Daily reports, test data, deviation closure, approved settings and signed SAT record | Provide operators, quality coverage, utilities, approved materials and release authority |
| Warranty and after-sales | Start point, duration, exclusions, response route, remote access, site-visit terms, parts responsibility and escalation | Support contacts, manual set, backups, recommended spares and closed handover actions | Maintain approved settings, records, safe access, preventive work and evidence for support cases |
Project-specific equipment proposal
Turn One Requirement Brief into a Comparable Complete-Line Scope
Send the country, source-water status, product, bottle and cap formats, target BPH, factory dimensions, utilities, final pack and intended startup date. Unknown inputs can remain marked for confirmation.
01 · Buyer or factory inputs
Information the decision needs
- Source-water basis and intended product
- Bottle material, volume, neck, cap, label and final pack data
- Required BPH and operating schedule
- Available factory and utility conditions
- Existing or quoted equipment list
- Required inspection, records, spare parts and service scope
02 · Operating objective
What completion should achieve
Confirm what each module must do, what it receives, what it passes downstream, which operating checks apply and which project data remain to be confirmed before final selection.
03 · Required controls
Turn the objective into controlled work
- 01
Water treatment: confirm input water, target basis, storage and demand interface
- 02
Bottle supply: confirm bottle/preform data, neck finish, compressed air and accumulation
- 03
Filling: confirm container, product, hygiene, fill and cap basis
- 04
Decoration: confirm container surface, label, code and inspection conditions
- 05
Packing: confirm pack pattern, material, line rate, handling and warehouse interface
- 06
Conveyors and controls: confirm elevations, accumulation, interlocks and stop logic
- 07
Utilities and support: confirm operating demand, quality, connections, drainage, laboratory and spares
04 · Factory interfaces
What connects to this decision
- Product-water supply and storage to filler demand
- Blower or bottle feed to filler infeed and accumulation
- Bottle/neck/cap to rinsing, filling and sealing parts
- Wet container condition to label adhesion and coding
- Filler discharge to conveyor, labeler, packer and warehouse handling
- Machine demand to electrical, air, water, drainage and environmental conditions
05 · Evidence to collect
Records that make review possible
- Project-specific technical offer
- General arrangement and interface drawings
- Confirmed utility schedule
- Bottle, neck, cap and label drawings
- Control and interlock description
- FAT and acceptance basis
- Manuals, spare-parts list and maintenance information
06 · Common failure modes
Do not confuse a pattern with a confirmed cause
1Comparing only rated BPH while interfaces use different bases
2Applying catalog reference values as final project commitments
3Ignoring conveyor, dryer, inspection or packing constraints
4Assuming utility availability without load and quality evidence
5Leaving operator and maintenance tasks outside the equipment review
07 · Responsibility boundary
Name who confirms each part
| Role | Possible responsibility in this stage |
|---|---|
| Buyer | Provide product, packaging, output, factory, utility and responsibility inputs. |
| Selected manufacturers | Confirm final models, performance basis, utilities, dimensions, materials, documents and acceptance conditions. |
| Local contractors | Confirm building, services, installation and interfaces within their scope. |
| Allot Tech | Coordinate project requirements and selected manufacturing resources according to the agreed scope. |
08 · Completion criteria
Evidence that the stage can advance
- Every module has a confirmed function and boundary
- Upstream and downstream interfaces use controlled data
- Catalog data are labeled as reference rather than final
- Utility and maintenance needs are recorded
- The signed technical and commercial agreement owns final conditions
Contact and support
Questions operating teams ask
Which machines are essential in a PET water bottling factory?
The usual functional chain is water treatment and storage, preform-to-bottle production or empty-bottle feeding, air conveying, rinsing-filling-capping, bottle drying, labeling, coding, inspection, packing and finished-pack conveying. Compressors, chillers, electrical distribution, drainage, laboratory checks and spare parts may also be necessary.
Should a water bottling factory quotation include the complete line?
Only if the written quotation clearly lists every included module, excluded local work, utility boundary, documentation, services, spare parts, installation responsibility and acceptance basis. A filling-machine quotation should not be treated as a complete-factory proposal.
Are catalog capacities final guarantees?
No. Catalog values are reference data. Final output, bottle basis, utilities, configuration, services and acceptance criteria must be confirmed in the signed project documents.
Is the filler always the factory constraint?
No. Bottle supply, product-water flow, labels, packing, conveyors, utilities, materials, quality holds, operators or maintenance can constrain saleable output.
Does Allot Tech claim every item is made in one owned factory?
No. Allot Tech coordinates project requirements and selected manufacturing resources. The approved supplier and responsibility structure is project-specific.
How do I choose a water bottling factory equipment supplier?
Issue the same controlled requirement to each supplier, then compare the complete equipment boundary, line interfaces, documented project evidence, factory acceptance test, installation and commissioning responsibility, training, manuals, spares, response route and written exclusions. Do not select on headline price or rated BPH alone.
What should a factory acceptance test cover for a water bottling line?
The signed FAT plan should name the available product or test medium, bottle formats, run conditions, duration, measurements, safety and functional checks, sample disposition, deviations, retest rules, records and the items that remain for site acceptance. The exact plan is project-specific.
Editorial responsibility: Allot Tech (Suzhou) Co., Ltd. · Last updated .